water based industrial lubricants and their role in casting die casting forging and extrusion

Introduction: The Critical Role of Lubricants in Thermal and Metal Forming Industries
In various industrial sectors such as die casting, aluminum casting, forging, extrusion, and even certain machining processes, the presence of an appropriate lubricant determines the difference between a successful production cycle and a defective process.
Lubricants are not only responsible for preventing molten metal from sticking, but they must also:
-
control die temperature
-
reduce friction
-
decrease tool wear
-
enhance the quality of the final product
-
reduce energy consumption and production time
Among all types of lubricants, water-based lubricants have gained a special position. These lubricants are not only highly advanced in terms of performance, but also offer significant environmental and economic advantages.
In this article, we examine all scientific, industrial, and practical aspects of water-based lubricants—with a level of detail typically found only in academic resources and technical catalogues of major manufacturers.
Chapter 1: What Are Water-Based Lubricants? – Scientific Definition
Water-based lubricants are emulsions or suspensions in which water acts as the carrier or continuous phase.
Active ingredients such as:
-
graphite
-
boron nitride (BN)
-
silica (SiO₂)
-
alumina (Al₂O₃)
-
molybdenum disulfide (MoS₂) — in certain formulations
-
emulsifiers and binders
are dispersed within water to form a stable mixture.
This system ensures:
-
uniform film formation on dies
-
reduced molten metal adhesion
-
delayed die wear
-
consistent cooling behavior
For this reason, water-based lubricants have replaced oil-based ones in nearly all modern die-casting, gravity-casting, and hot-forging production lines.
Chapter 2: Chemical Structure of Water-Based Lubricants – A Deeper Look
To understand the function of a water-based lubricant, one must analyze its components scientifically.
1) The Aqueous Phase (Water Phase)
Water serves as the main carrier and is responsible for:
-
temperature reduction
-
transporting active ingredients
-
promoting dispersion
-
lowering viscosity
Deionized (DI) or RO water is typically used to prevent scaling or residue formation.
2) Solid Lubricants (Active Solid Phase)
Graphite
-
Temperature resistance up to 1000°C
-
Layered structure → low friction
-
Suitable for aluminum casting and forging
Boron Nitride (BN)
-
Temperature resistance 1200–1400°C
-
Excellent anti-stick properties
-
Best choice for aluminum die casting
-
High thermal conductivity → improved die temperature control
Zircon / Zircon Silicate
-
Resistance up to 1600°C
-
Ideal for cast iron and steel foundries
Alumina (Al₂O₃)
-
High thermal shock resistance
-
Suitable for heavy-duty forging and hot dies
3) Binders and Emulsifiers
Their functions include:
-
stabilizing the mixture
-
preventing sedimentation
-
improving adhesion to die surfaces
Common types include:
-
polyvinyl alcohol
-
industrial gums
-
silicates
-
phosphates
4) Functional Additives
Such as:
-
defoamers
-
antioxidants
-
anti-corrosion agents
-
pH stabilizers
These ensure long-term stability throughout continuous production cycles.
Chapter 3: Why Have Water-Based Lubricants Become So Popular? – Comparison with Oil-Based Lubricants
Oil-based lubricants were widely used in the past, but they suffered from major drawbacks:
❌ heavy smoke emission
❌ fire hazard
❌ carbon buildup
❌ high consumption
❌ difficult cleaning
❌ poor workplace environment
These issues led industries toward water-based solutions.
Key Advantages of Water-Based Lubricants
✅ non-flammable
✅ smoke-free
✅ dilutable (1:5 to 1:40)
✅ superior thermal control
✅ environmentally friendly
✅ lower lubricant consumption
✅ no carbon deposits
✅ extended die life
Chapter 4: Types of Water-Based Lubricants by Industry
1) Water-Based Lubricants for Die Casting
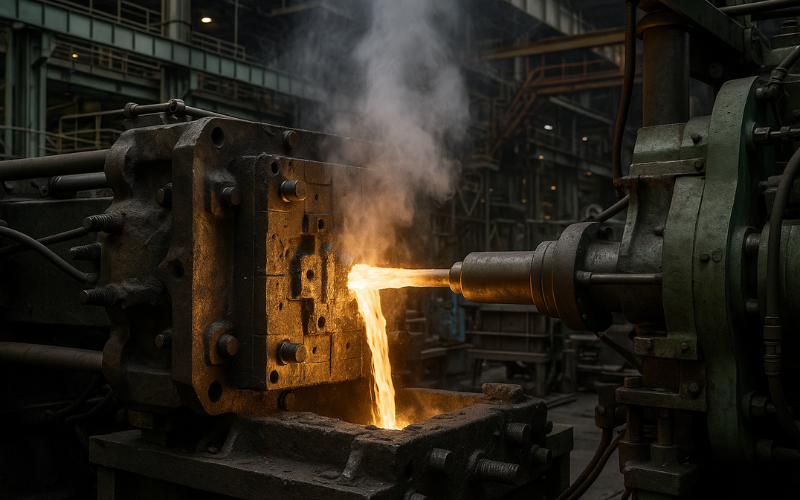
Die casting is one of the most thermally demanding processes. Dies undergo extreme thermal shock in every cycle, and lubricants must withstand this.
Functions
-
reducing aluminum adhesion
-
uniform die cooling
-
lowering gas porosity
-
lubricating ejector pins
-
preventing thermal fatigue cracks
-
improving surface finish
Formulation Components
-
micronized graphite
-
pure BN
-
silicone emulsions
-
industrial defoamers
-
water volatility controllers
2) Water-Based Lubricants for Forging
In hot forging of steel, lubricants must withstand 1000–1200°C.
Functions
-
preventing adhesion of hot steel
-
reducing die friction
-
helping fill the die cavity
-
preventing hot cracks
Main Components
-
graphite
-
sodium silicate
-
phosphates
-
alumina
3) Water-Based Lubricants for Extrusion
Especially for hot aluminum extrusion, lubrication must be precise and uniform.
Functions
-
reducing extrusion force
-
lowering frictional heat
-
preventing billet sticking
-
improving surface finish of profiles
Typical Additives
-
BN
-
graphite
-
phosphates
-
gel-like structures for improved adhesion
4) Water-Based Coatings for Ladles and Melt-Handling Tools
These include refractory coatings for:
-
ladles
-
crucibles
-
scoops
-
runners
Functions of Ladle Coatings
-
preventing reactions between melt and ladle
-
reducing contamination
-
preventing oxidation
-
maintaining proper thermal resistance
Commonly based on:
-
zircon
-
BN
-
graphite
-
refractory minerals
Chapter 5: How Water-Based Lubricants Work When Applied to a Hot Die
When a water-based lubricant is sprayed onto a hot die, several key phenomena occur:
1) Rapid Evaporation of Water
Water instantly evaporates, cooling the surface.
2) Deposition of Solid Particles
Active solids (graphite, BN) remain on the die surface as a thin film.
3) Formation of a Uniform Layer
This layer provides:
-
anti-stick performance
-
thermal resistance
-
friction reduction
4) Protection Against Thermal Shock
The die uses this film as a protective buffer against molten metal impact.
5) Reduction of Wear
Solid lubricants significantly reduce abrasive wear.
Chapter 6: Factors Affecting Spray Quality
Spray performance in die casting and forging is as important as the lubricant itself.
Critical parameters:
-
Air and Water Pressure
Low → insufficient coverage
High → film washes away -
Spray Nozzle Angle
Optimal angle: 90° -
Nozzle-to-Die Distance
Typically 30–50 cm -
Spray Time
Too long → excessive die cooling
Too short → sticking problems -
Dilution Ratio and Lubricant Type
Chapter 7: Dilution Ratio (Mixing Formula)
Proper dilution is crucial.
Heavy Die Casting:
1:20 to 1:40 (1 liter lubricant + 20–40 liters water)
Light Die Casting:
1:10 to 1:20
Hot Forging:
1:5 to 1:12
Extrusion:
1:3 to 1:8
Ladle Coating:
Undiluted or 1:1 to 1:3
Chapter 8: Common Problems and Their Causes
| Problem | Cause |
|---|---|
| Aluminum sticking to die | incorrect dilution, poor spray pattern |
| Gas porosity | uneven coating, overly cold die |
| Die corrosion | lack of corrosion inhibitors |
| Sedimentation in tank | insufficient agitation, weak emulsifier |
| Excessive evaporation | high air pressure, not enough active solids |
Chapter 9: Correct Application Method
-
precise dilution according to instructions
-
uniform mixing
-
filtering lubricant before entering tank
-
test spraying before production
-
monitoring film thickness
-
controlling ambient temperature and humidity
Chapter 10: The Future of Water-Based Lubricants
Industry trends are moving toward:
-
intelligent smart lubricants
-
nano-graphite coatings
-
carbon-free formulations
-
lubricants optimized for robotic spraying
-
coatings for complex 3D die geometries
Within the next decade, oil-based lubricants will be almost entirely phased out.
Final Summary
Water-based lubricants have become the most essential consumables in die casting, casting, forging, and extrusion due to:
-
high performance
-
thermal stability
-
zero smoke and zero fire risk
-
reduced consumption
-
extended die life
-
precise thermal control
-
improved product quality
They are now a cornerstone of modern thermal processing and metal forming industries.



No comment for this post.